Understanding the exact Broken Star Anise Extraction & Spice Facts is absolutely essential for commercial spice grinders, international culinary buyers, and industrial pharmaceutical facilities who want to comprehend why this specific botanical variant dictates the global commercial anise economy. Unlike visually perfect whole stars used for aesthetic retail purposes, this fragmented pod is meticulously sifted to provide a highly potent, oil-dense ingredient that serves as the economic backbone of mass-market retail powders and advanced essential oil distillation.
For international procurement teams and supply chain managers looking to capitalize on this immense global demand, reviewing the operational logistics of the Broken Star Anise Bulk Export Supply Line is the mandatory next strategic step. However, before investing in bulk container loads, buyers must fully understand the physical, chemical, and agricultural components that make this specific grade the most heavily utilized star anise commodity across commercial manufacturing sectors.
Table of Contents
-
Core Botanical Profile and Sizing Characteristics
-
The Harvesting and Fragmentation Process
-
Chemical Profile: Essential Broken Star Anise Extraction & Spice Facts
-
Shikimic Acid and Industrial Synergy
-
Conclusion

Core Botanical Profile and Sizing Characteristics
When analyzing the massive commercial success of this globally traded commodity, the primary differentiator lies in the precise, volume-optimized post-harvest processing of the Illicium verum tree’s fruit.
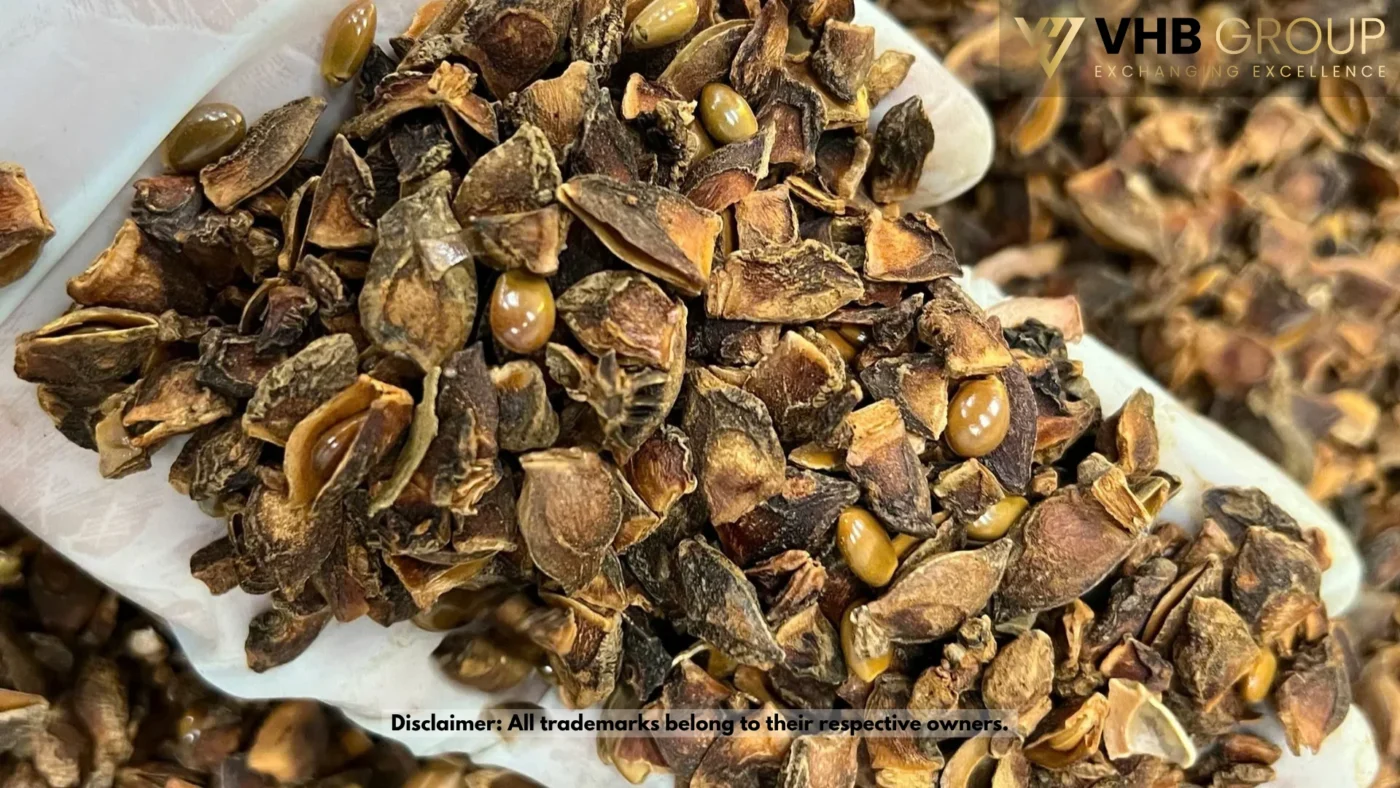
Broken star anise consists of the fragmented, irregularly shaped pieces of the woody pericarp and the inner seeds that naturally shatter during the harvesting, drying, and packing process of premium whole stars. Rather than being a low-quality waste product, premium broken star anise is sourced from the exact same mature trees as the high-end whole pods, ensuring it retains the massive essential oil content required for industrial processing.
The Harvesting and Fragmentation Process
A critical element within the agricultural profile is the crop’s unique mechanical cleaning and optical sorting requirement, heavily focused in the processing hubs of Lang Son, Vietnam, and Guangxi, China.
Once the green pods are harvested, they are spread out on massive patios to dry under the intense equatorial sun. During this sun-drying phase, the moisture content is rapidly reduced down to a strict maximum of 13.5%. The dried, hardened pods that shatter are collected and passed through vibrating mechanical sieves to separate the usable broken pieces from dust, stems, and dirt. This sifting ensures that the final broken grade remains highly pure, maximizing the yield for extraction facilities.
Chemical Profile: Essential Broken Star Anise Extraction & Spice Facts
The most distinctive physical characteristic of the ingredient upon grinding or steaming is its robust, aggressively sweet-licorice flavor profile which translates perfectly into culinary powders and liquid extracts.
Balancing Pungency and Alkaloids
Because the product is 100% natural, the Broken Star Anise Extraction & Spice Facts matrix is heavily determined by its Volatile Oil (VO) content. Standard commercial broken star anise contains roughly 3.0% to 5.0% VO. When loaded into a steam distillation vat, the broken nature of the pods drastically increases the surface area exposed to the steam, accelerating the release of anethole, the essential oil responsible for the signature licorice aroma heavily utilized in cosmetics, oral care, and flavoring.
Shikimic Acid and Industrial Synergy
To fully grasp the commercial appeal, pharmaceutical extraction facilities and commercial blenders must analyze the macro-chemical profile. The fragmented pod is carefully calibrated by nature for optimal chemical synthesis.
| Chemical Component | Content Range | Primary Function in Culinary/Pharma Use |
| Volatile Oil (VO) | 3.0% – 5.0%+ | The primary indicator of quality, dictating the total aromatic strength. |
| Shikimic Acid | 3.0% – 7.0% | A highly prized industrial precursor used in the synthesis of antiviral medications (like Tamiflu). |
| Anethole | 80% – 90% of VO | The specific organic compound responsible for the signature flavor. |
| Moisture Content | < 13.5% | Strictly controlled to prevent mold (fungus) and ensure safe global export. |

Conclusion
Mastering the foundational botanical and processing facts is the definitive key to understanding its unstoppable global commercial velocity in mass-market food production and pharmaceutical synthesis. From the careful management of high volatile oil yields to the precision mechanics of industrial volume sorting and sifting, every single element of the broken star anise crop is designed to deliver a highly functional, perfectly consistent, and economical experience. For international distributors and commercial grinders, stocking this authentic agricultural product guarantees access to a highly liquid, highly profitable supply chain. Contact your preferred procurement partner today to secure your wholesale agricultural allocation.
Broken Star Anise Facts FAQ
Disclaimer: Unless otherwise stated, the images used in this article are the property of their respective owners. We do not claim ownership of any third-party images featured, and they are used here strictly for informational and educational purposes. If you are the copyright holder and wish to have an image removed, please contact us.